
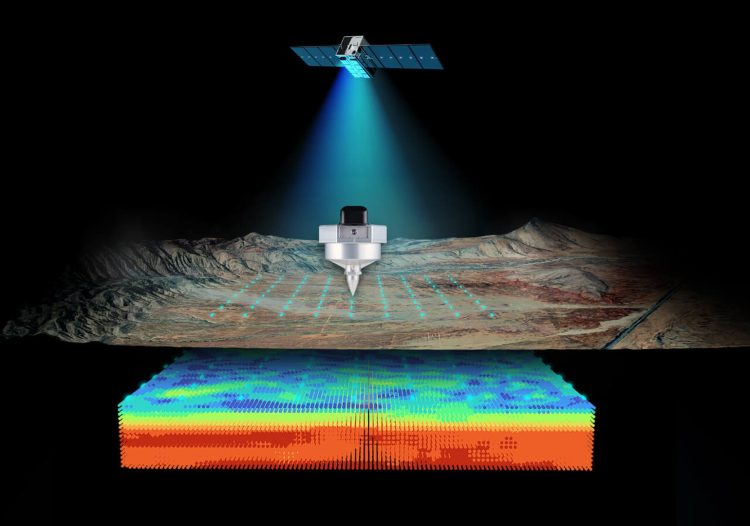
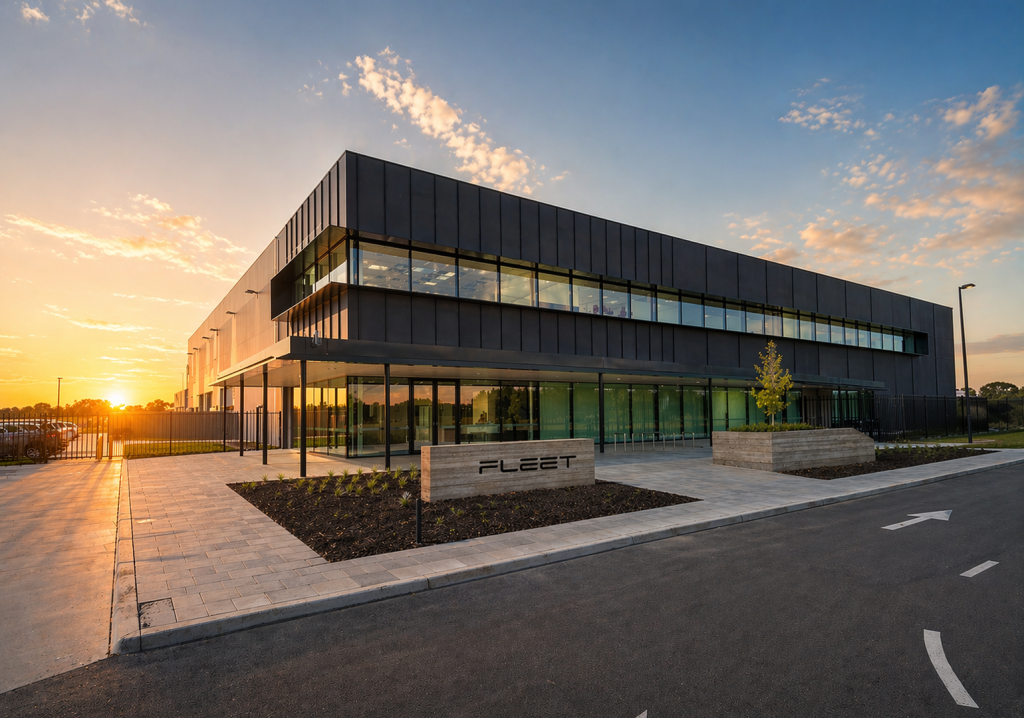
That principle has ensured that prototypes were not stuck in commercial cul-de-sacs, but on a path towards repeatable production. Equally critical was the company’s approach to overcoming the dreaded first-mover problem.
“Trust came from putting real hardware in the field and proving reliability under operational conditions, not lab assumptions,” Tata Nardini said.
These arrangements accelerated Fleet Space’s transition from promising technology to commercialisation.
“Early customer application with customers such as Rio Tinto was critical. It validated the technology and accelerated our ability to invest in larger-scale deployments on Earth and in space.”
The lesson Fleet Space draws from that experience is one many only recognise in hindsight.
“Design for scale earlier than feels comfortable. The transition from demo to deployment happens when engineering decisions are grounded in manufacturing, reliability, and customer outcomes – not just technical success.”
Scale of ambition
Not all innovations begin from a position where scale can be assumed. Micro-X, which designs and manufactures carbon-nanotube X-ray technology, operates under the unique constraint of manufacturing products where the science itself is still developing.
Conventional X-ray systems rely on heated filaments to generate electrons, which generate significant heat.
“For decades, the research was stuck, because you simply couldn’t draw out enough current without the nanotubes breaking down,” Micro-X COO Anthony Skeats said.
Solving this problem required not only new materials, but a new understanding of how millions of nanoscale emitters behave collectively under stress.
Micro-X replaces them with cold-cathode carbon nanotube field emitters, which generate electrons using electric fields rather than heat. This means smaller, lighter, faster and more controllable X-ray tubes. Typical mobile units are around 25 kg and Micro-X’s are 2.5 kg. Conventional CT tubes are usually 15-20 kg but Micro-X’s weigh 200 g.
“The carbon nanotubes are the invention,” Skeats said. “The innovation is how we use them – and that’s what eventually has to bring in revenue.”
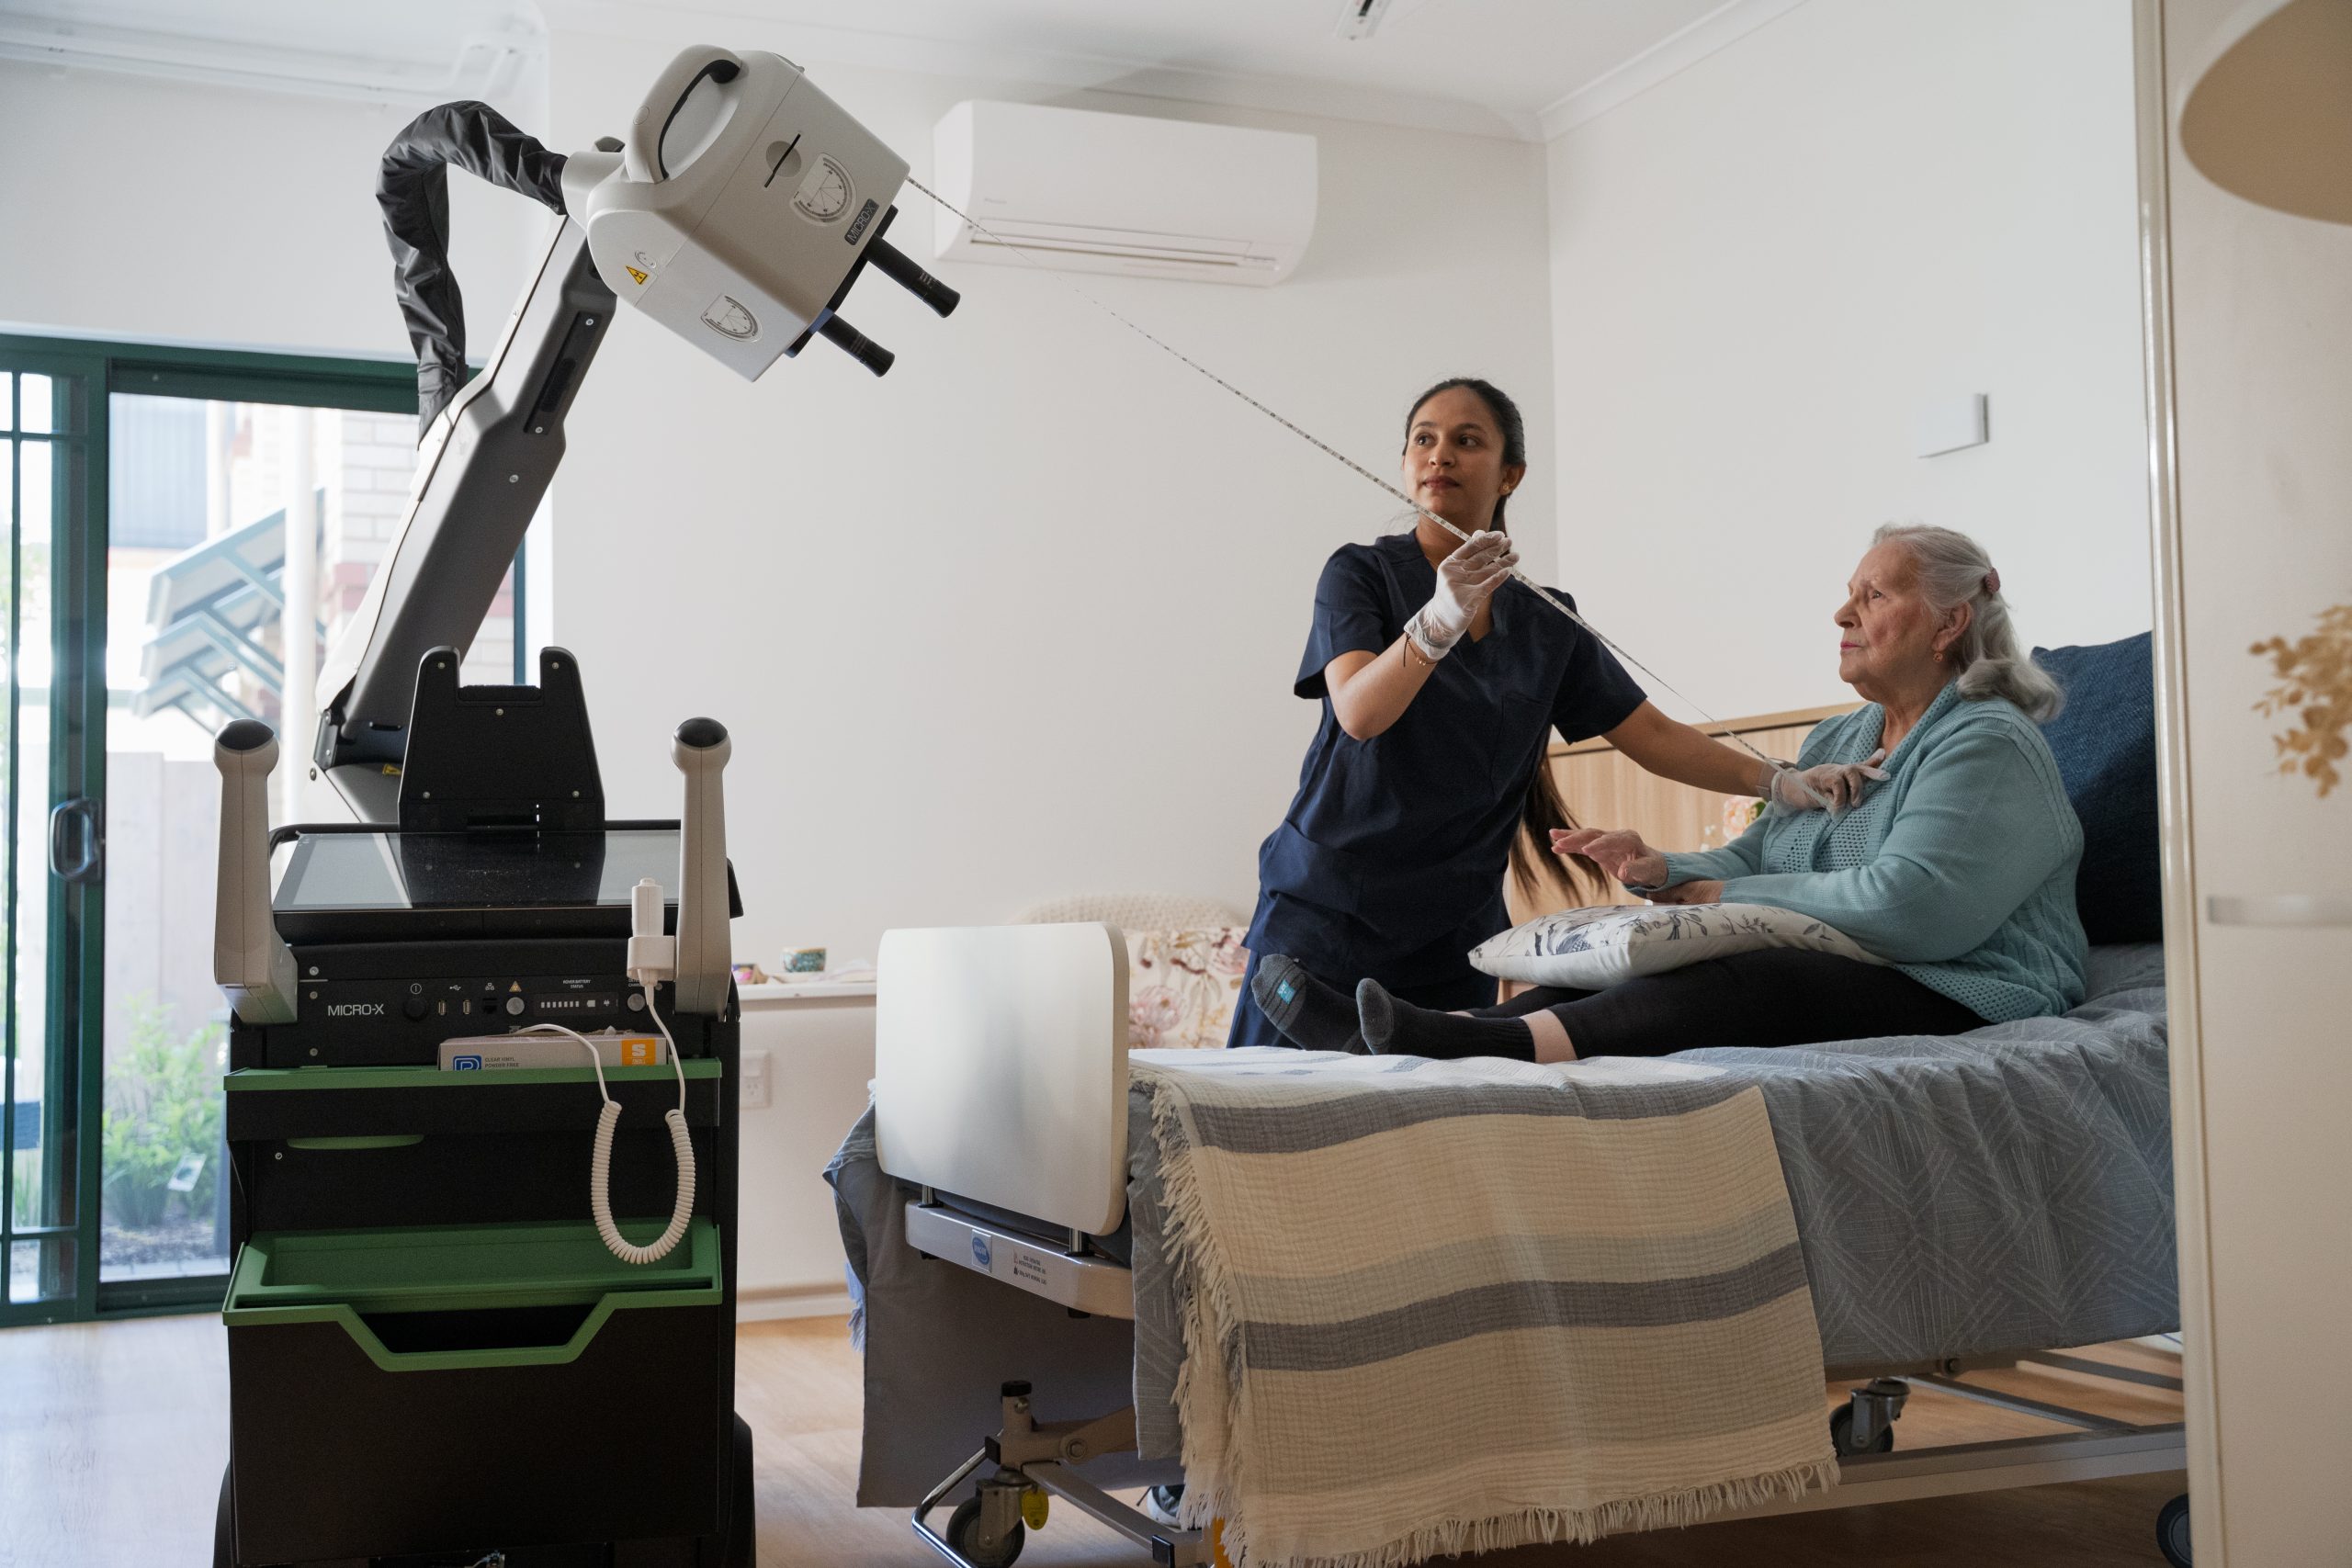
Unlike more mature technologies, where product development follows proven principles, Micro-X had to take what Skeats described as an “extraordinary risk” to develop its core technology and its commercial products in parallel. That meant leaps such as committing to manufacturing pathways, certification processes and market entry while the technology is still being engineered.
Working with such highly specialised technologies presents another problem: finding early adopters in Australia can be difficult. “When you go overseas, the first question is always: who’s using this in your own country?”
The experience illustrates a recurring pattern: when technologies are hardest, the gap between technical success and commercial scale is amplified. And there are still fundamental problems in committing to making advanced products onshore.
“The quality of manufacturing in Australia is extremely good, but suffers from the demise of things like the automotive industry … the biggest challenge we face in Australia is that tyranny of distance.”
READ how Micro-X rethought the 100-year-old X-ray tube.
Automating success
If Micro-X highlights the difficulty of scaling scientific breakthroughs, Conry Tech highlights different pressure points in turning domestic innovation into mass production.
The Melbourne-based company is developing the BullAnt, an air-conditioning system designed to radically reduce energy use in commercial buildings by decentralising and transferring heat rather than relying on traditional energy-intensive cooling units. Conry believes it could halve energy bills and eliminate billions of tonnes of carbon emissions.
The technical ambition is significant, but the decision that has most shaped Conry’s trajectory is where, and how, that technology is built.
“We’re foolishly patriotic,” co-founder Sam Ringwaldt said of the firm’s commitment to manufacture in Australia, despite strong incentives to offshore.
But Ringwaldt wouldn’t do anything differently, as he sees controlling the manufacturing process as the first step in retaining control of their IP.
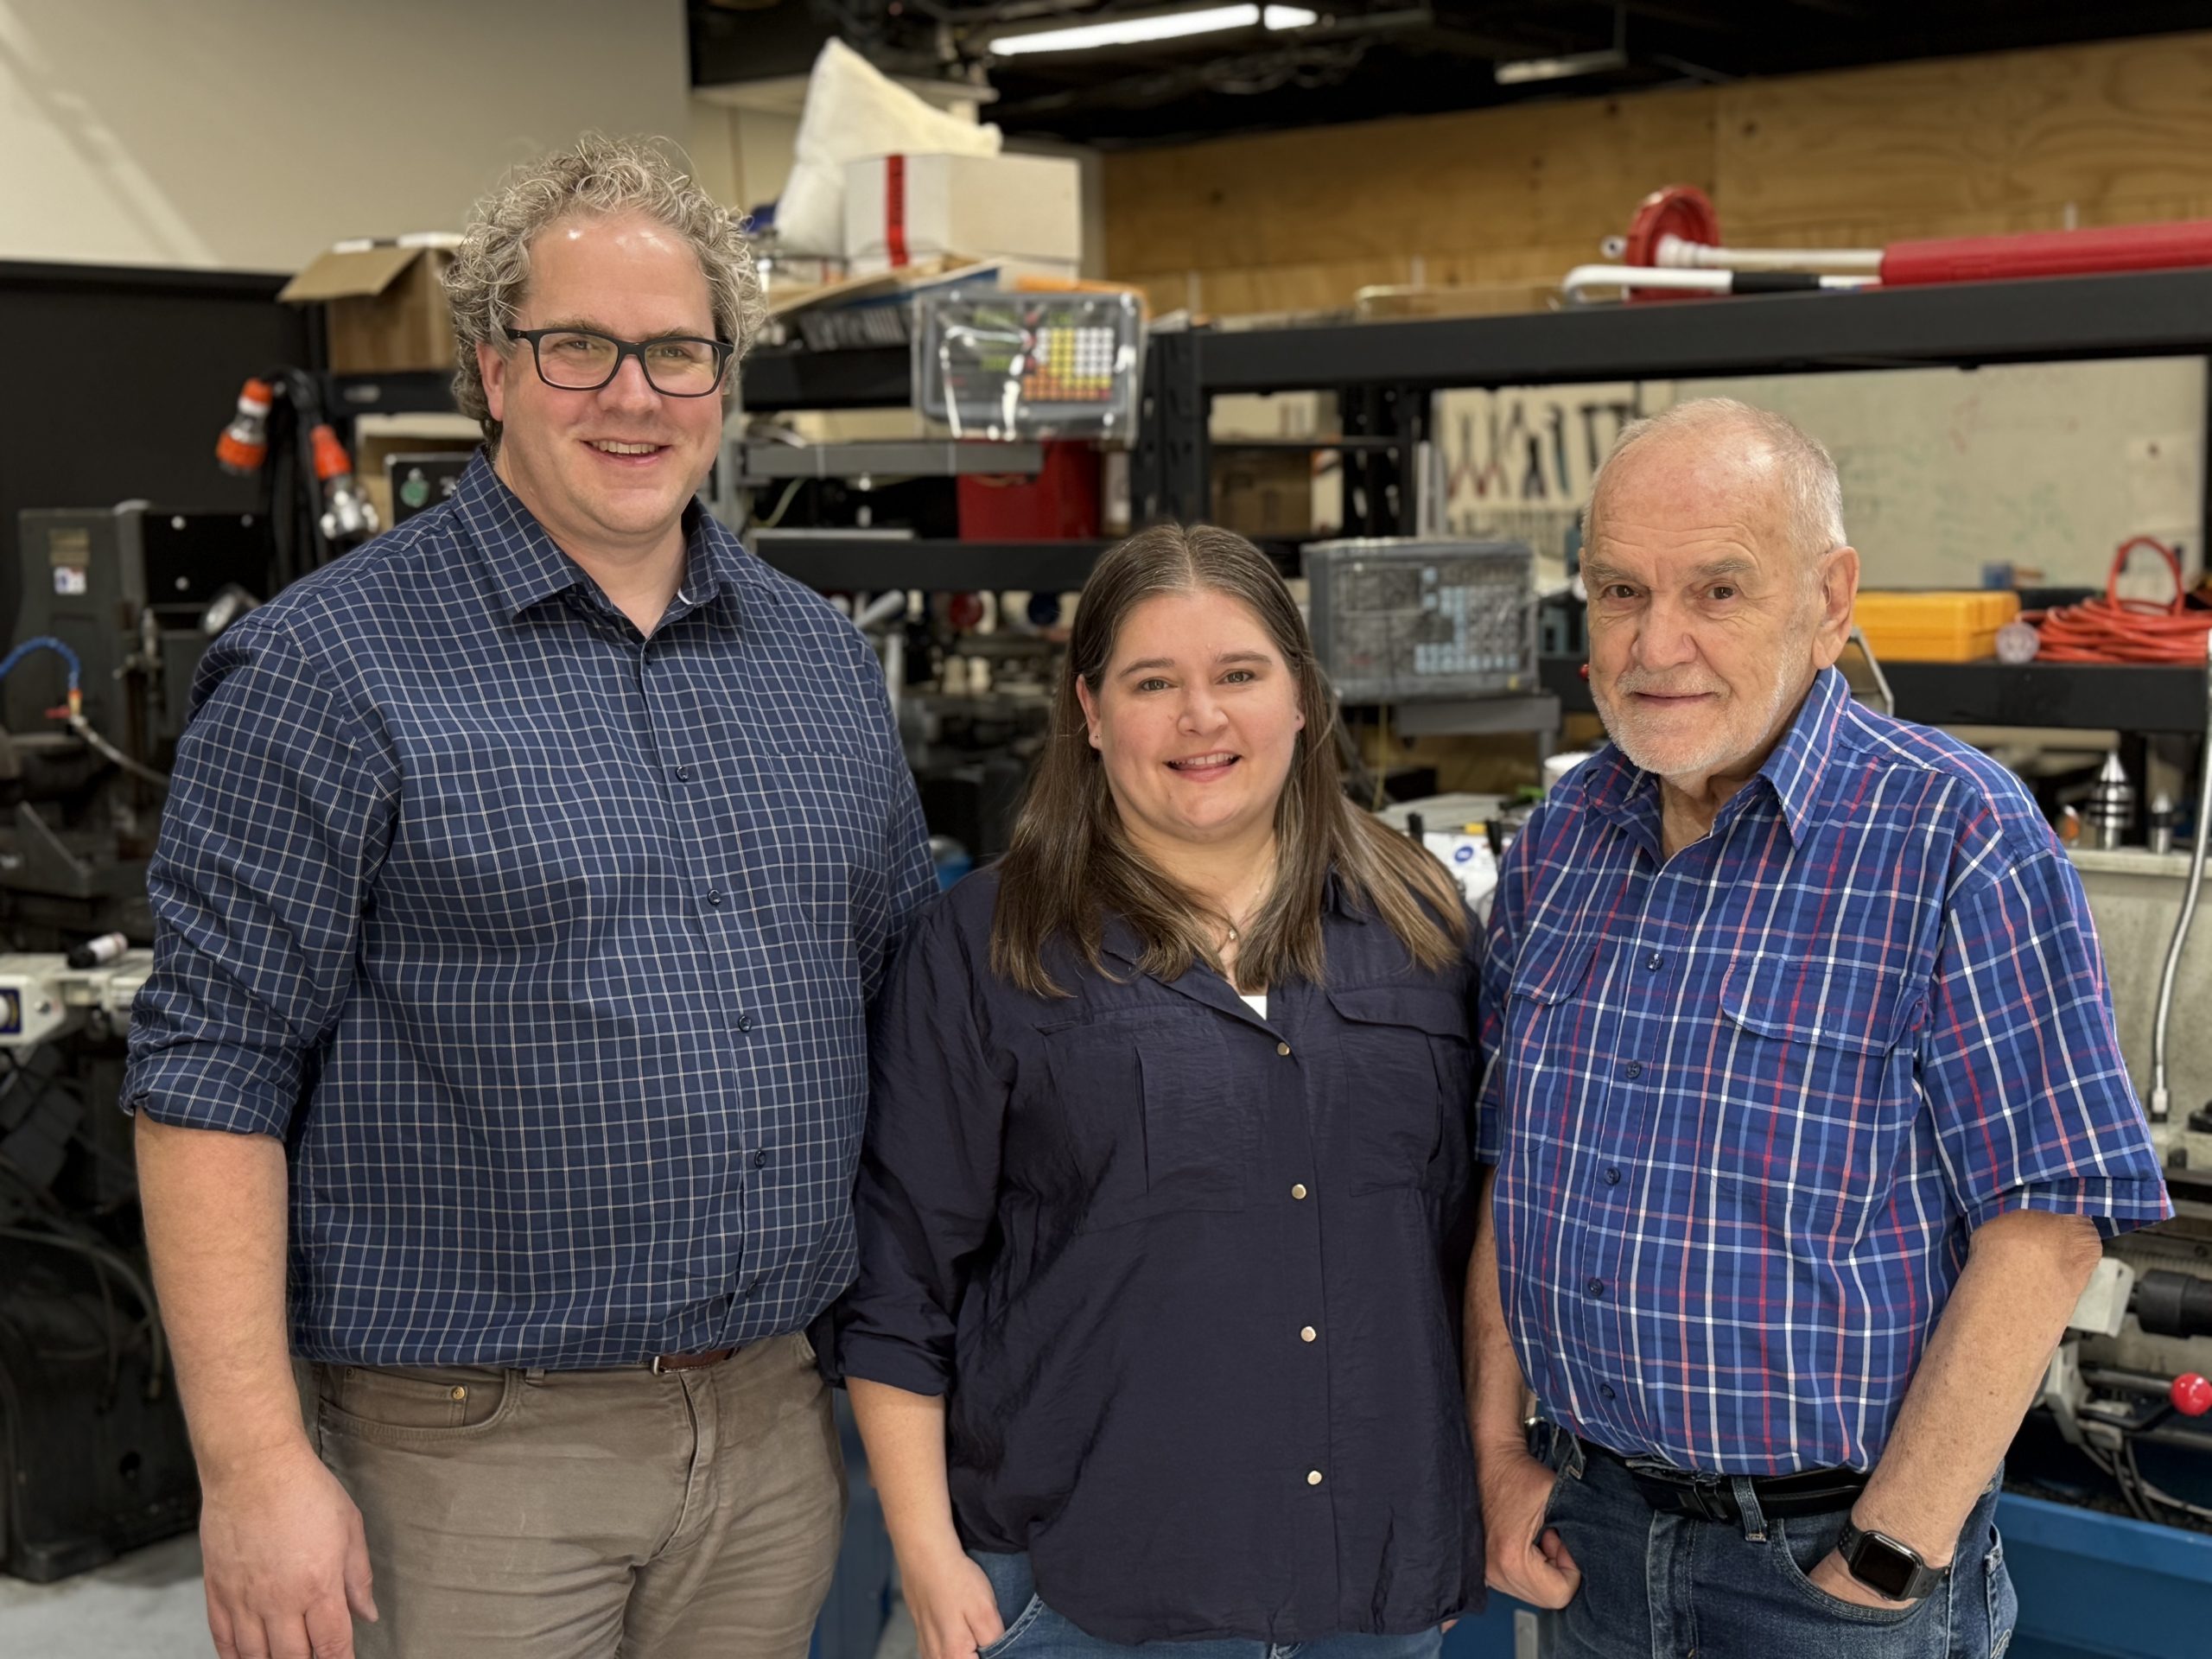
Company co-founder Ron Conry, who has had 40 factories in 10 different countries, added: “Australia still has a competitive advantage in terms of our education system, where we produce people who can think and question and problem-solve on the shop floor.”
Despite the need to protect IP, Ringwaldt said the obstacles to manufacturing in Australia are well understood. Capital is harder to secure, labour costs are higher and the domestic market is small. Investors expect “global aspirations”, yet value companies as if their ceiling were the Australian market alone.
“If you want to stay in Australia, you need to build a high-quality team and start manufacturing locally. Otherwise, be prepared to give up a lot more of your equity locally, or capital will pull your business offshore.”
The resulting funding gap means businesses need to give away more equity than similar firms overseas. Government assistance is similarly constrained, tending to operate on risk matrixes that are oriented towards commercial success.
Conry Tech’s response has been engineering-led. Rather than attempting to compete with low-cost and subsidised manufacturing jurisdictions on labour, it has designed the BullAnt system with advanced manufacturing practices, such as 3D printing and additive manufacturing, and ensuring processes minimise labour.
“For manufacturing to work in Australia, you have to design for automation from the very start.”
READ about Conry Tech’s innovation in air conditioning.
Automation over offshoring
Sydney’s RØDE Microphones is an example of a global company that has moved production onshore to Australia as a deliberate engineering and operational strategy.
Synonymous with high-quality audio, powering everything from podcasts to major films, RØDE designs, tests and manufactures microphones and audio products that compete with – and often outperform – counterparts made overseas.
Needing to significantly improve product quality to compete against Chinese firms with cheaper labour with closer proximity to parts, RØDE invested millions in automated machinery that makes high-precision parts, quickly and at high volume – and with a greater degree of accuracy than those hand-made overseas.
The strategy has also enabled RØDE to respond to market pressures with unusual speed. When threatened by a rival’s wireless microphone product, the company redesigned and brought an advanced replacement to market in just 100 business days. Such a business decision was only possible thanks to the integration of engineering, tooling and assembly under one roof.
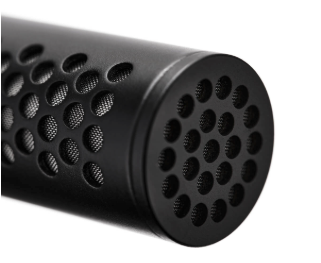
Where it once sourced many of its components in China, since bringing capsule production in-house, RØDE has dramatically tightened quality control, with rejection rates falling from around 50 per cent to less than 3 per cent today. The early success of bringing some of its key production in-house is leading the company to consider what else can be brought back to Sydney, as it aims to move more production under its own control, with its own machines.
Early investments in production technology – including machines for printed circuit board assembly and precision lapping equipment for capsule manufacture – have allowed engineers to iterate rapidly between design and manufacture. Previously, when the company depended on overseas contractors, it faced months between ordering and sampling, and experienced price and quality risks once parts were in the hands of third parties.
Operating their own manufacturing means engineers can flesh out ideas and be producing concepts within days.
It’s already reaping the rewards. According to RØDE founder Peter Freedman, onshore, automated manufacturing now means “we’re cheaper and better than China”.
READ: Yes, Australia can manufacture, and it’s up to our engineers
Stall patterns
Taken together, the experiences of the above countries point to patterns that distinguish Australian innovations that scale from those that stall. In each case, engineers realised early that their technologies would need to confront Australia’s structural barriers through bold engineering choices.
Australia’s challenge, then, is not a lack of ideas, talent or technical ambition. It is a lack of sustained support for the most demanding phase of engineering work: the transition from something that functions to something that can be built, certified, sold and supported at scale.
For engineers, the implications are clear: scaling innovation is a key component of the engineering discipline itself. When manufacturability, reliability and deployment are treated as solvable design problems rather than external barriers, Australian innovations are far more likely to thrive.
This article was originally published in the May 2026 edition of create with the headline “Made in Australia”.
Celebrate the engineers driving the next Australian innovations at an upcoming local event organised for the Engineers Australia Excellence Awards.