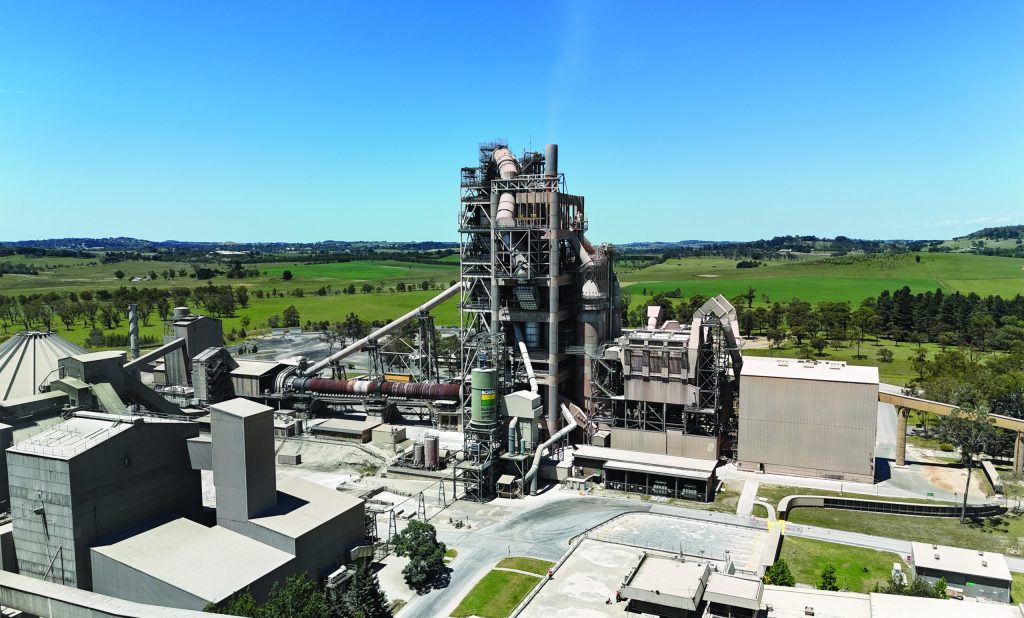
A chlorine bypass system at Berrima Cement Works will double the use of alternative fuels at the plant over the next three years, reducing its carbon emissions by up to 75,000 t annually.
Boral’s Berrima Cement Works supplies approximately 40 per cent of the cement used in NSW and the ACT, making it a critical asset in Australia’s construction industry.
The technology behind a chlorine bypass, commissioned in 2024, will enable the firm to meet its decarbonisation targets and reduce its reliance on emissions-intensive fuels such as coal, driving smarter, cleaner cement manufacturing.
The integration of the chlorine bypass will allow the cement works to increase its use of alternative fuels to 60 per cent by 2026. Additionally, the system contributes to a reduction in the emissions intensity of clinker production by up to 11 per cent due to decreased calcination emissions and some improved thermal efficiency.
Managing the transition
Boral made a strategic decision in 2018 to pivot away from coal in favour of biomass and other zero-carbon fuels, a course which a number of cement plants around the world had already adopted.
“We decided on the bypass because we have one kiln which produces about 1.5 million t of clinker annually, which then makes the cement,” Rajeev Ramankutty, Boral’s Executive General Manager of Cement, told create.
“Every tonne of cement produced at Berrima generates around 683 kg of carbon dioxide, with 65 per cent coming from the decomposition of limestone and the other 35 per cent from fuel.”
With the industry standard for clinker usually at 800 kg of carbon dioxide, the facility was already ahead, but it wanted to continue to reduce its carbon footprint.
Ramankutty said Boral began its transition to using waste-derived fuels conservatively. “We used wood from construction demolition waste, which is quite a benign fuel to burn as it doesn’t have many nasties in it – but the availability of this fuel is limited.”
Tasked with reaching 60 per cent coal substitution by 2026, the engineers had to consider waste-derived sources of fuel, such as PVC plastics, which presented a technical hurdle due to the substantial amounts of chlorides and sulfides they contain.
“When burning different fuels in the kiln, there is a lot of volatility, particularly related to chloride, sulfide and the alkali cycles,” Ramankutty said. “They’re fine at high temperatures, but when operating at cooler temperatures, potassium and sodium chlorides become solid – which builds up deposits in the system.”
Such build-ups are extremely difficult to manage, causing blockages that can interrupt operations or even force a full kiln shutdown. They also present a safety risk because the materials are so hot they flow like water, and have been responsible for severe burn incidents at other facilities around the world.
The nitty gritty
Managing and mitigating chloride content in gas streams is crucial for both operational efficiency and environmental compliance in cement manufacturing.
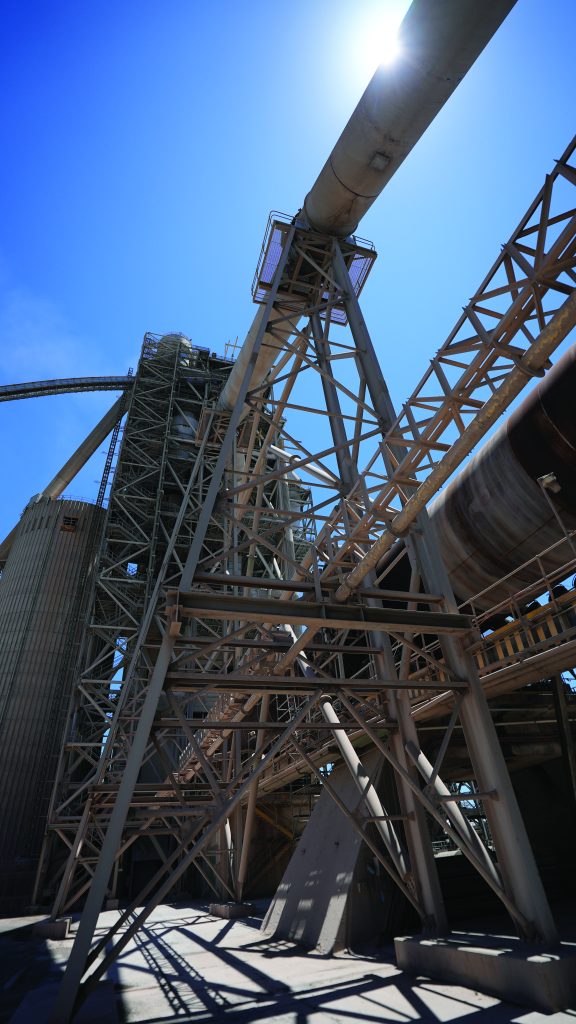
“The chlorine bypass process begins by extracting the gas stream, which contains chlorides among other compounds. This gas exits the kiln system at extremely high temperatures, typically around 1,200°C.
“It then goes through an air quenching system housed in a mixing chamber, where it is mixed with atmospheric air, and the temperature drops to about 400°C. A vertical heat exchanger then further reduces the temperature to less than 200°C.”
This staged cooling is essential because chlorides, which are initially present in gaseous form, begin to solidify once the temperature drops below their melting point of around 700°C.
Once solidified, the chloride particles can be efficiently captured using a bag filter system. The resulting dust can then be recovered by shaking the filter to release the dust.
“The reason why you need to cool down is that bag filters don’t like very high temperatures,” Ramankutty said. The recovered dust, rich in chlorides, is then reintegrated into the cement grinding process, further reducing plant waste. “While there are regulatory limits on chloride content in cement, this system allows us to remain well within those standards.”
Fueling the fire
Moving from coal to alternative fuels in cement production has three key environmental benefits: the straight reduction in carbon emissions from tripling the use of waste-derived fuels, transforming waste liabilities into energy assets, and easing the burden on landfill systems.
Presently, the Berrima plant uses a mixture of products, including wood chips, used automobile tyres, and refuse-derived fuel, the latter of which is responsible for most of the chlorides.
With emissions reduction on track, the engineers are now turning to a broader range of materials that would otherwise be destined for disposal. “We’ll be looking at things like recovered industrial waste oil, and shredding plastic wrappers and other light packaging materials into very fine particles for combustion,” Ramankutty said.
The diversity of alternative fuels helps in securing their long-term supply. The bypass’s flexibility in being able to use any type of fuel also avoids build-up in the process, which is key to alternative fuel program success.
“The way to look at the bypass is that it is the key enabler in unlocking the potential of burning fuels,” Ramankutty said.
By allowing the kiln to tolerate fuels with high chlorides, sulfides or other volatile contents, it ensures the safe processing of more difficult-to-handle waste, which it often considered undesirable due to the operational risks it poses.
This expands sourcing options and adds economic value.
“In some cases, we receive gate fees for accepting and processing specific waste fuels – otherwise it can cost between $200 and $300 per tonne just to put it in landfill.”
Burning ambitions
The benefits of the bypass system show it is more than just a technical upgrade – it’s an investment in long-term resilience. It allows the Berrima plant to burn a broader range of alternative fuels safely and efficiently, while cutting carbon emissions, reducing landfill pressure and creating new income streams.
After a feasibility study highlighted the benefits of the bypass system for the cement works, it required a substantial capital investment of around $20 million, with the NSW Government supporting the project with a grant amounting to almost a quarter of the cost.
Since the bypass came online, it has tripled the plant’s alternative fuel use to around 45 per cent, with a clear pathway to the 60 per cent target. In the process, it will help Boral to reach its 2030 decarbonisation targets.
However, Ramankutty said the engineers don’t intend to stop there.
“The pace at which we have moved is really impressive compared to [other] more mature countries which have gone down this path. Some European countries are burning 80-90 per cent waste fuel, and that’s where we want to be.”
This story was originally published in the August 2025 issue of create with the headline “Cementing resilience”.